Plant manager
“Why did we lose output this week, and will it happen again?”
- Downtime by asset and cause, not by shift note.
- Early warnings on machines drifting out of normal.
- One view of availability across lines and sites.


 Riyadh, Saudi Arabia
Manufacturing & Industry
Machines, utilities and mobile plant reporting condition before they stop.
/ The context /
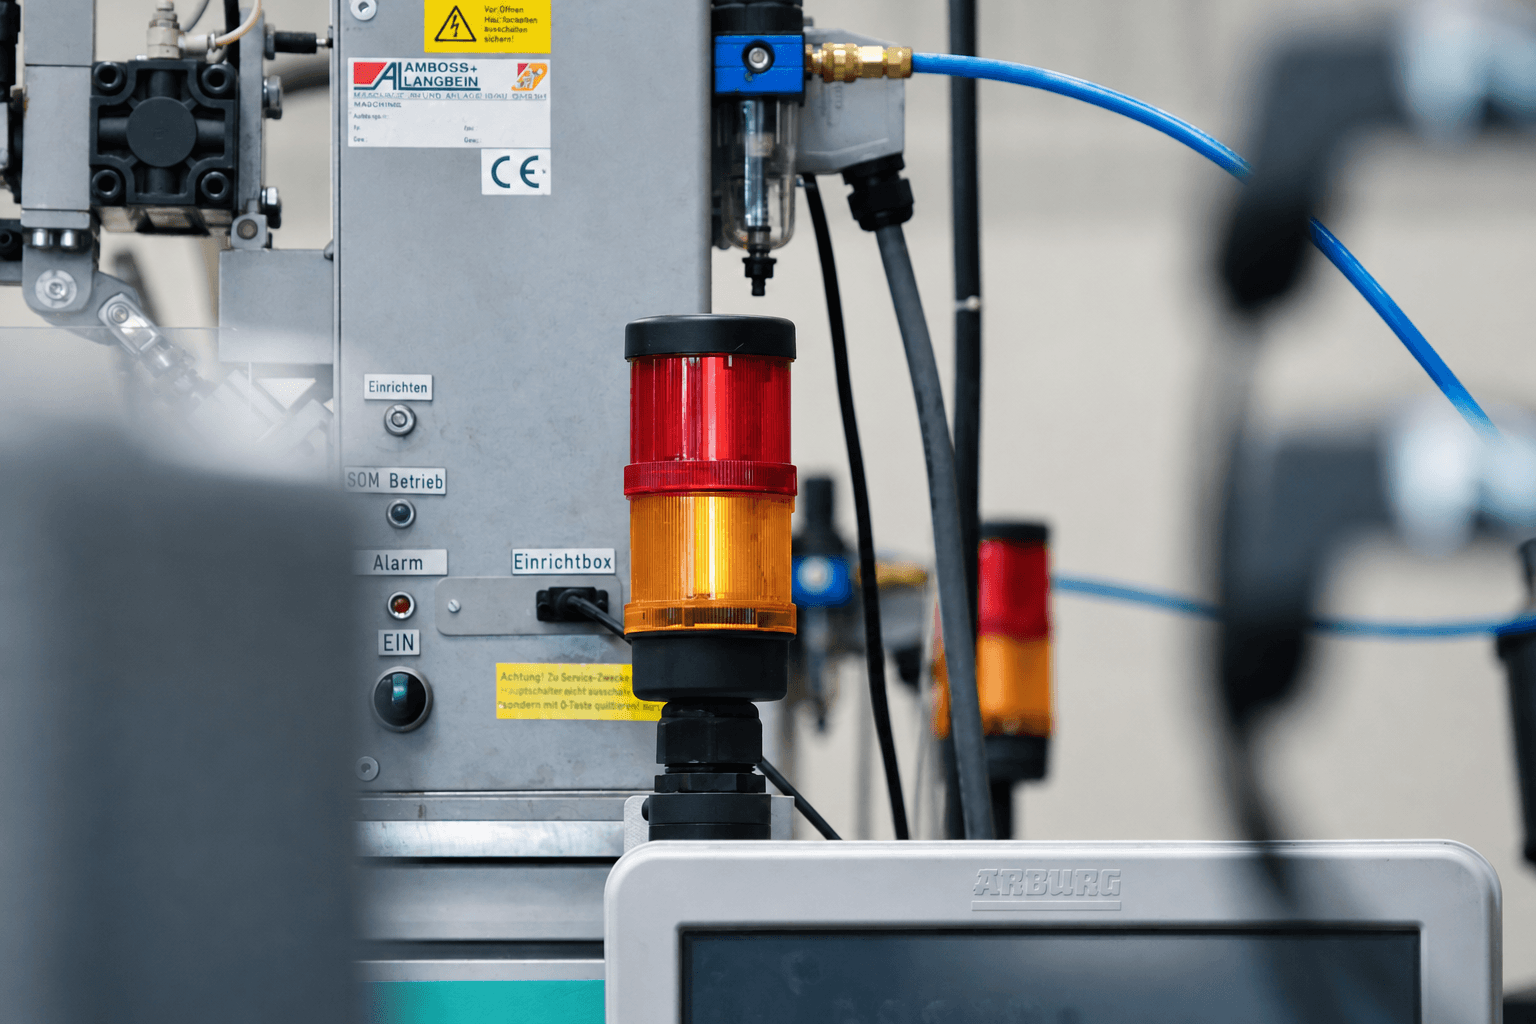
Plants run on equipment that warns before it fails, and on maintenance schedules built around dates rather than condition. Money goes on servicing healthy machines while output is lost to the one that was drifting.
Connecting machines, utilities and mobile plant turns unplanned downtime into planned work, and gives a plant manager a defensible number for a problem now described with adjectives.
The National Industrial Development and Logistics Program is pushing more production into the Kingdom, and new plants are expected to run reliably from the first year.
Energy pricing reform has made consumption a real line in the plant budget, so compressed air, chillers and idle running show up in the cost per unit.
Experienced technicians are hard to find and harder to keep, so their time has to go to machines that need attention rather than routine checks.
/ The challenges /
Assets are serviced on fixed dates regardless of condition, so healthy machines are opened up while the one drifting out of tolerance waits for its slot.
Stoppages are logged by shift in notebooks or spreadsheets, so nobody can say what caused the last month of lost output.
Controllers already hold useful signals, but they sit on isolated SCADA screens where engineering and management never see them.
Leaking air lines, oversized chillers and equipment left running overnight cost money every hour. Without metering by area, the waste has no owner.
/ Where it shows up /
Each one runs on the same foundation, so the second costs a fraction of the first.
/ What we connect /
Whatever the brand, protocol or supplier, joined to the systems that already run the business.
/ By role /
Plant manager
Maintenance lead
Energy manager
Finance director
/ How we engage /
We walk the floor with maintenance and production, agree the critical assets, and check what PLC, SCADA and metering data exists.
Sensors go in where needed, existing controllers are read where possible, and a baseline is built per critical asset.
Alerts feed maintenance workflows so drift becomes a planned job, and stoppages and savings are reviewed against the baseline.
Further lines, utilities and sites join, ERP and CMMS are connected, and the plant runs the dashboards itself.
/ Compliance /
Confirm the exact format your authority requires and we map the export to it.
Production, energy and equipment records are structured to support the operational reporting industrial licence holders are asked to maintain.
Process and environmental conditions can be logged continuously, designed to support the quality records manufacturers keep against SASO product standards.
Operational technology is connected through segmented, read-only paths with logged access, designed to support alignment with the NCA Essential Cybersecurity Controls.
/ Security & sovereignty /
/ Built on IoT Cube /
Saudi distributor of IoT and telematics hardware: trackers, dashcams, sensors, RFID, routers and EV chargers, fitted and supported.
On-demand car care and vehicle maintenance, booked in a few taps at a chosen time and place.
AI assisted HR for the GCC: attendance, payroll, leave, requests, recruitment and the whole employee lifecycle.
/ Questions /
No. IoT Cube sits alongside existing SCADA and historians and reads the signals you already have. Sensors go in only where the data does not exist, such as vibration on older machines.
/ Other industries /
We will walk through your estate, the systems around it and where connecting it pays for itself first.